Page 10 of 10
Re: 646-75lbh Restoration
Posted: Mon Nov 09, 2026 7:40 pm
by Spike188
This morning I got around to taking the transaxle to a high-end welding shop that have used for major repairs over the years.It turns out that the scheduling technician a wheelhorse collector which led to over the top service. Between keeping the housing stub hot and cooling slowly and limited access to the area needing repaired, He advised against welding.
What the tech pointed out is that there can be a bit of shoulder left to stop the bushing against.
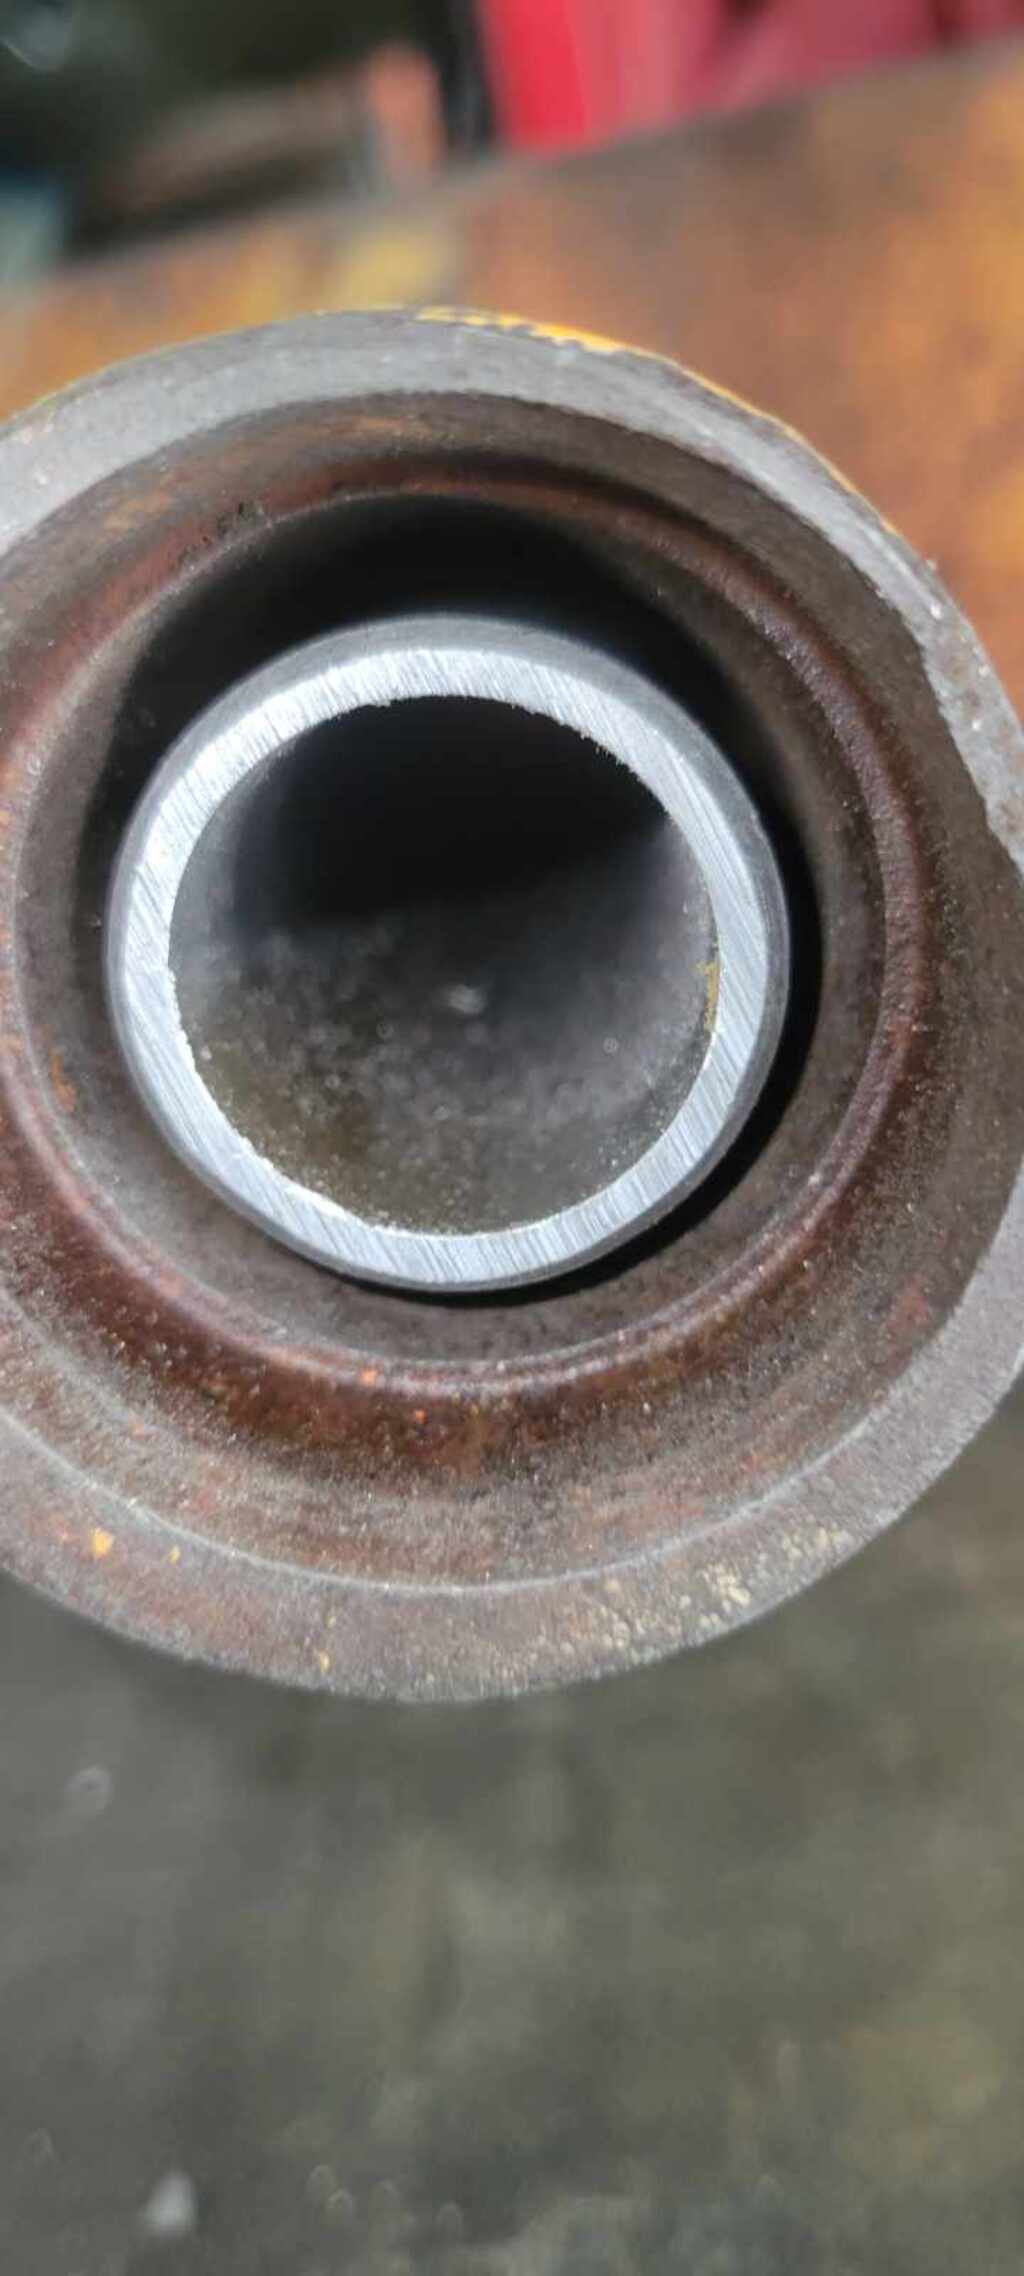
- Resized_20260821_152423.jpeg (88.96 KiB) Viewed 81 times
The approach now will be milling the bushing location round and concentric, after which a custom oilite bushing will be turned.
Re: 646-75lbh Restoration
Posted: Tue Nov 10, 2026 5:40 am
by DavidBarkey
Due to the reduced material on the pressure side of new bushing , I would recommend making a couple of heavy band clamps to clamp around the bearing area and spreading the load to the non-pressure side of the axle tube . If it was 200 , or 400 series it would not matter , but because it is a BH carrying a large load all the time I think it would be prudent .
Re: 646-75lbh Restoration
Posted: Tue Nov 10, 2026 7:03 am
by Spike188
@DavidBarkey I like that idea better than machining the exterior of the axle housing and sleeving it. My concern with machining a sleeve is making a stress relief taper where the sleeve meets the webbing on the housing.